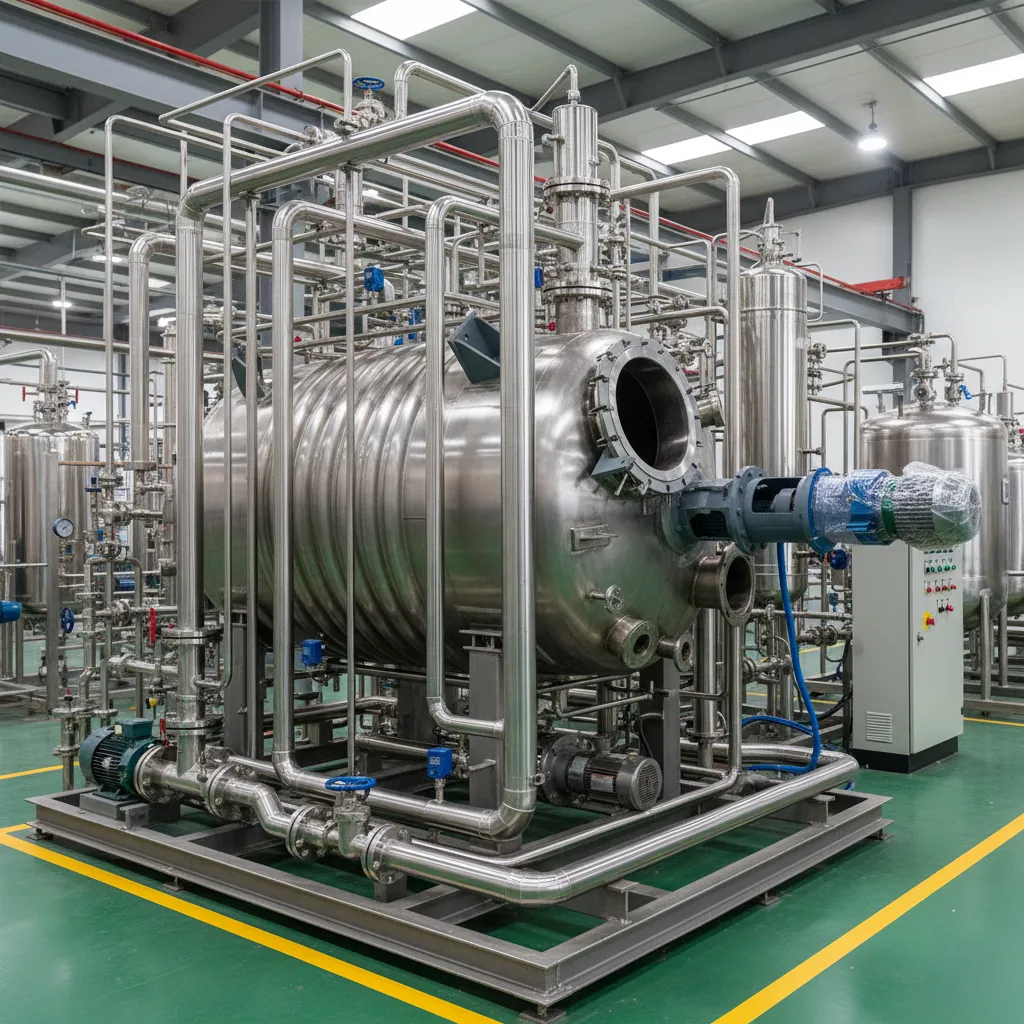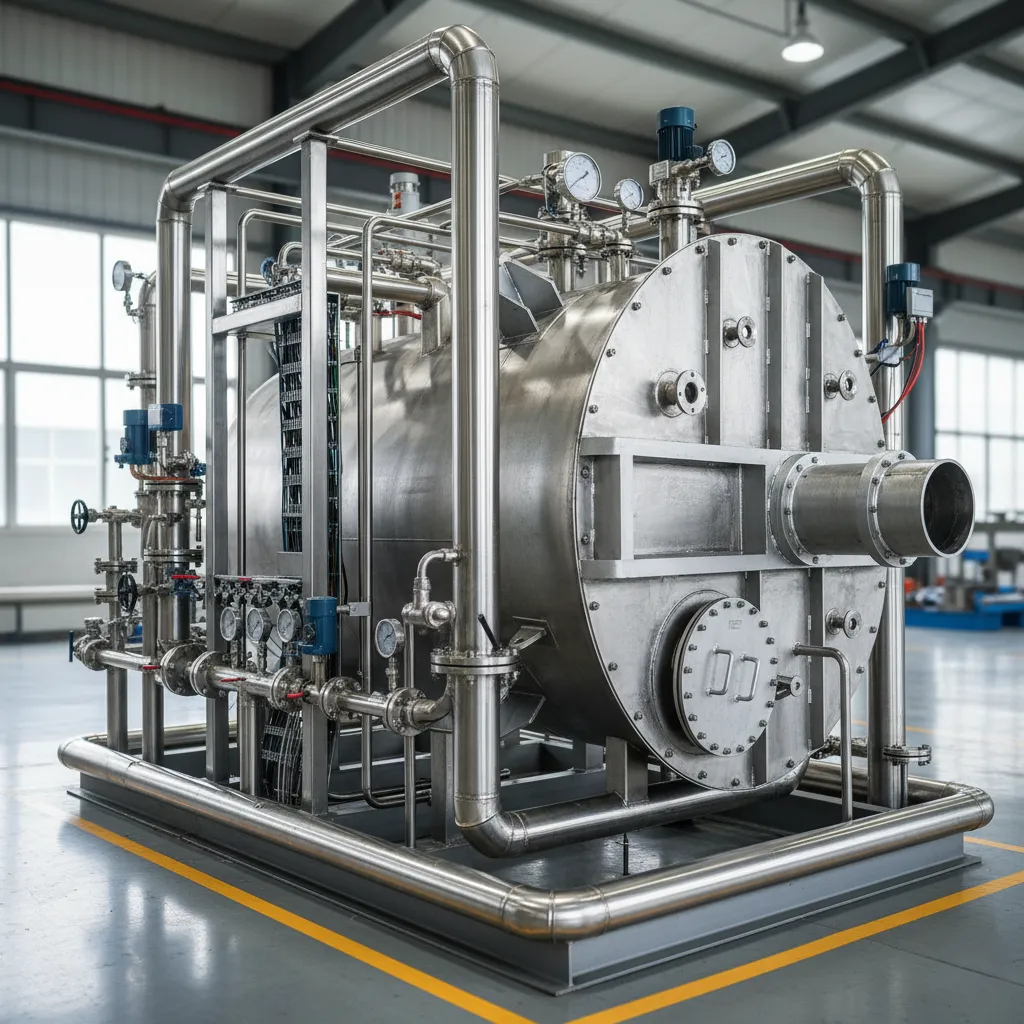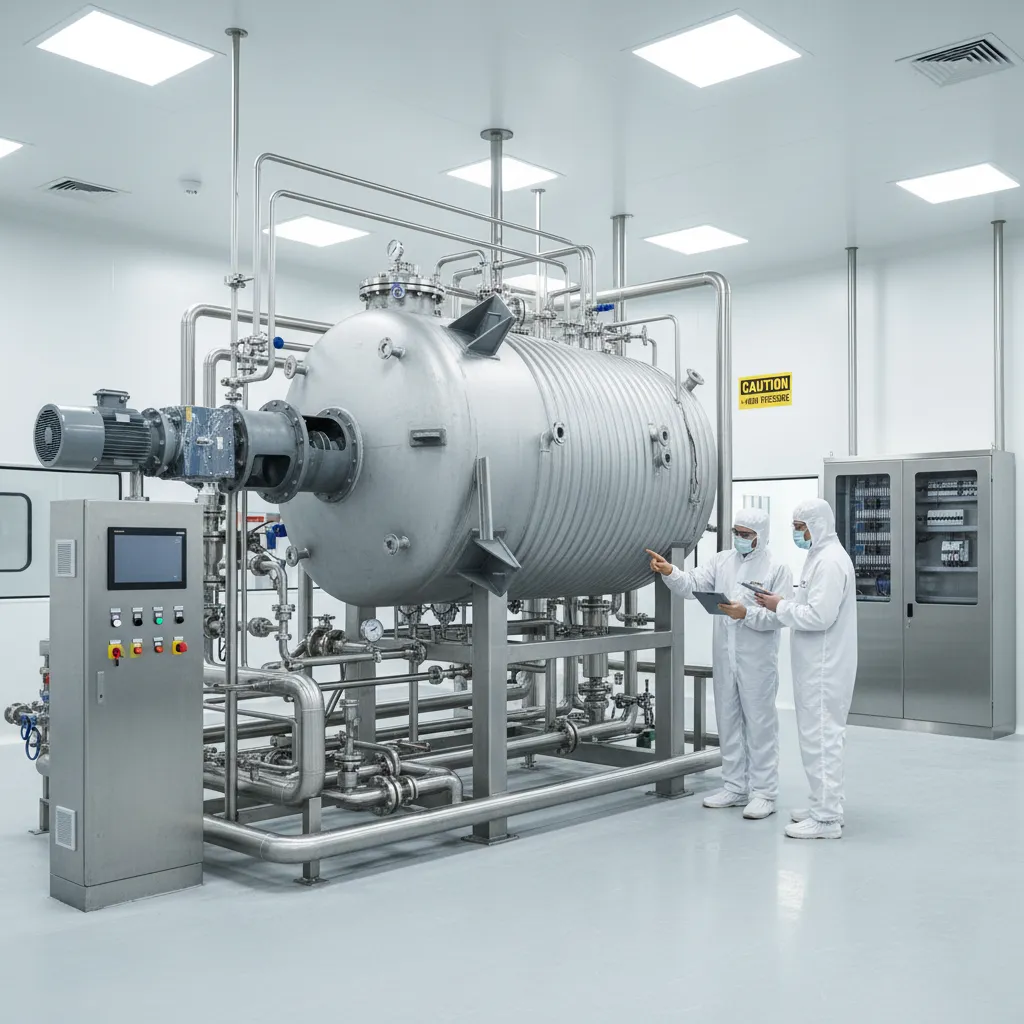
Stainless Steel Chemical Reactor

Stainless Steel Chemical Reactor
Reactors & Vessels

Stainless Steel Chemical Reactor

SS reactors for controlled chemical processing and reactions.

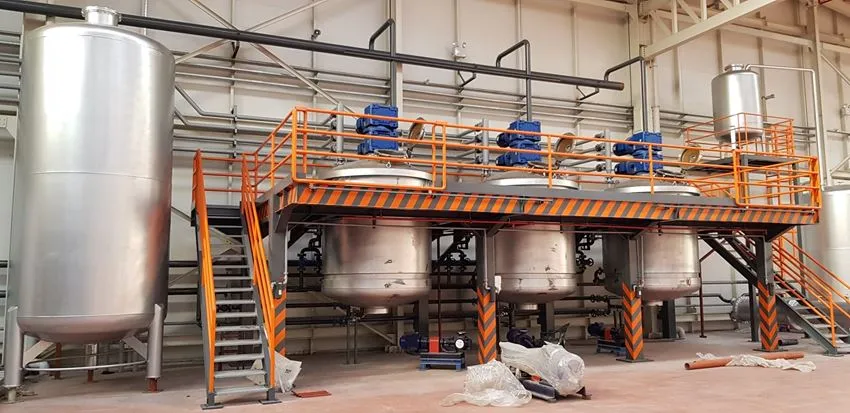
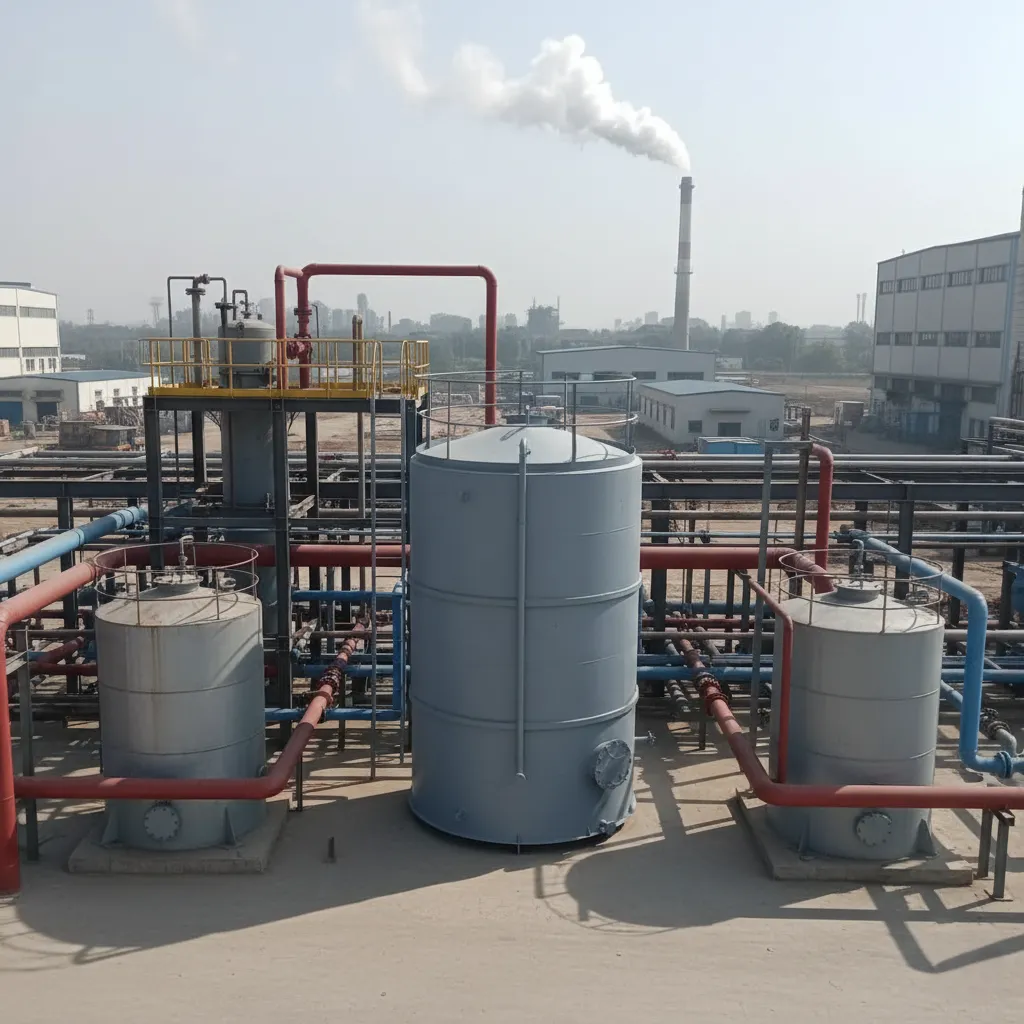
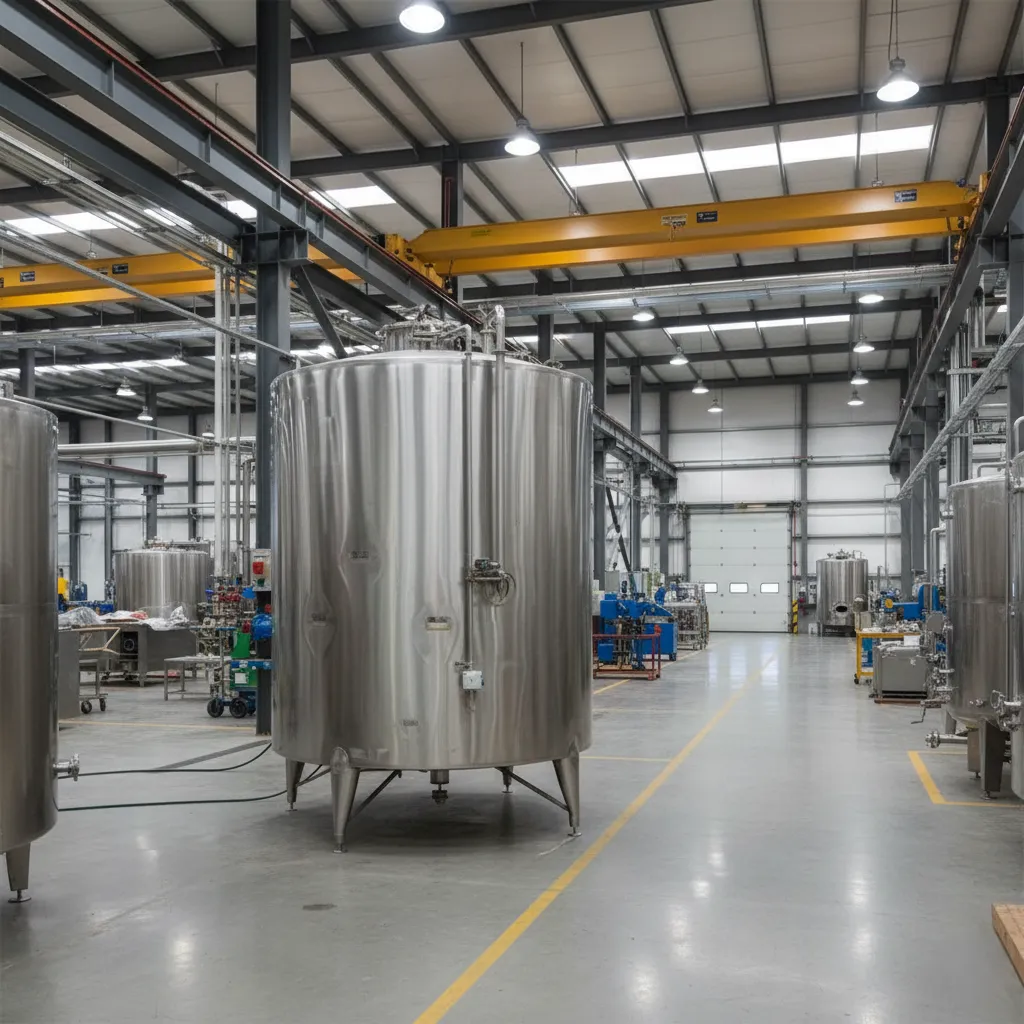
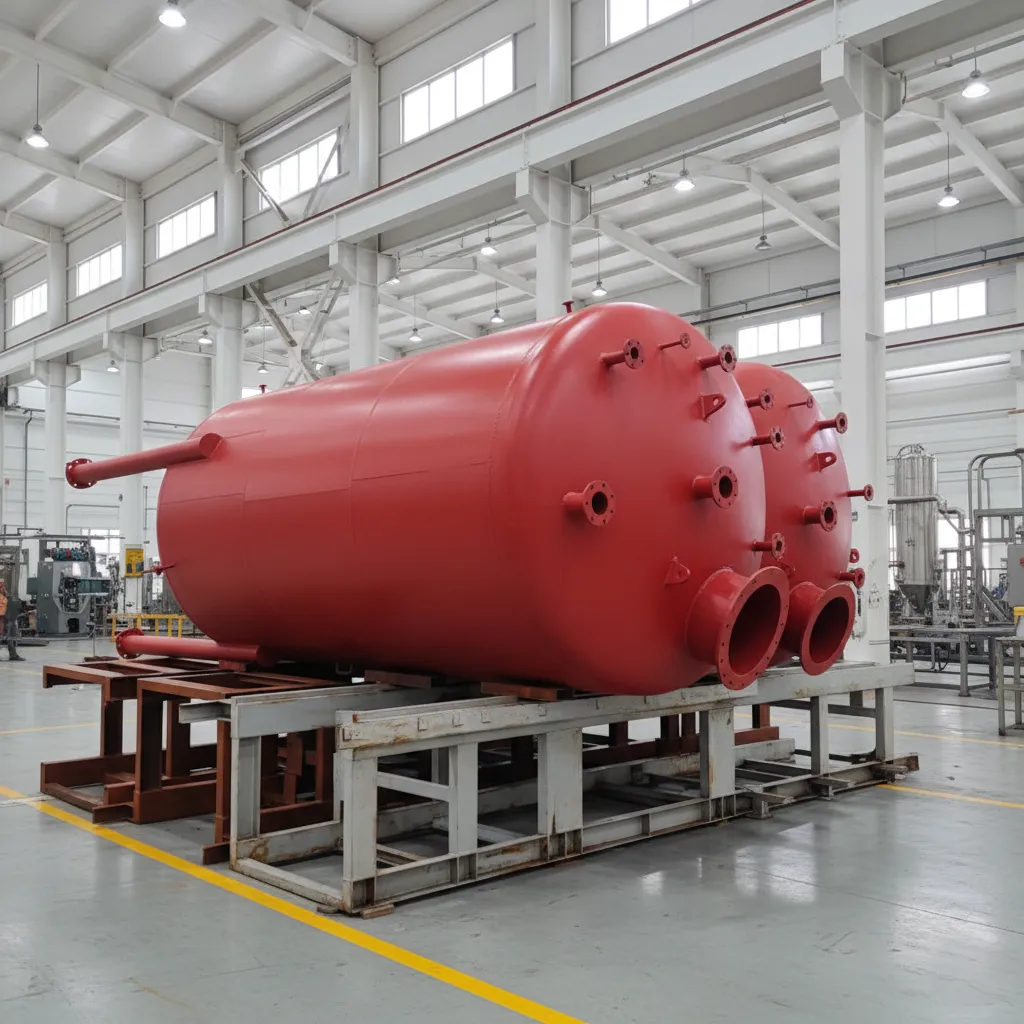
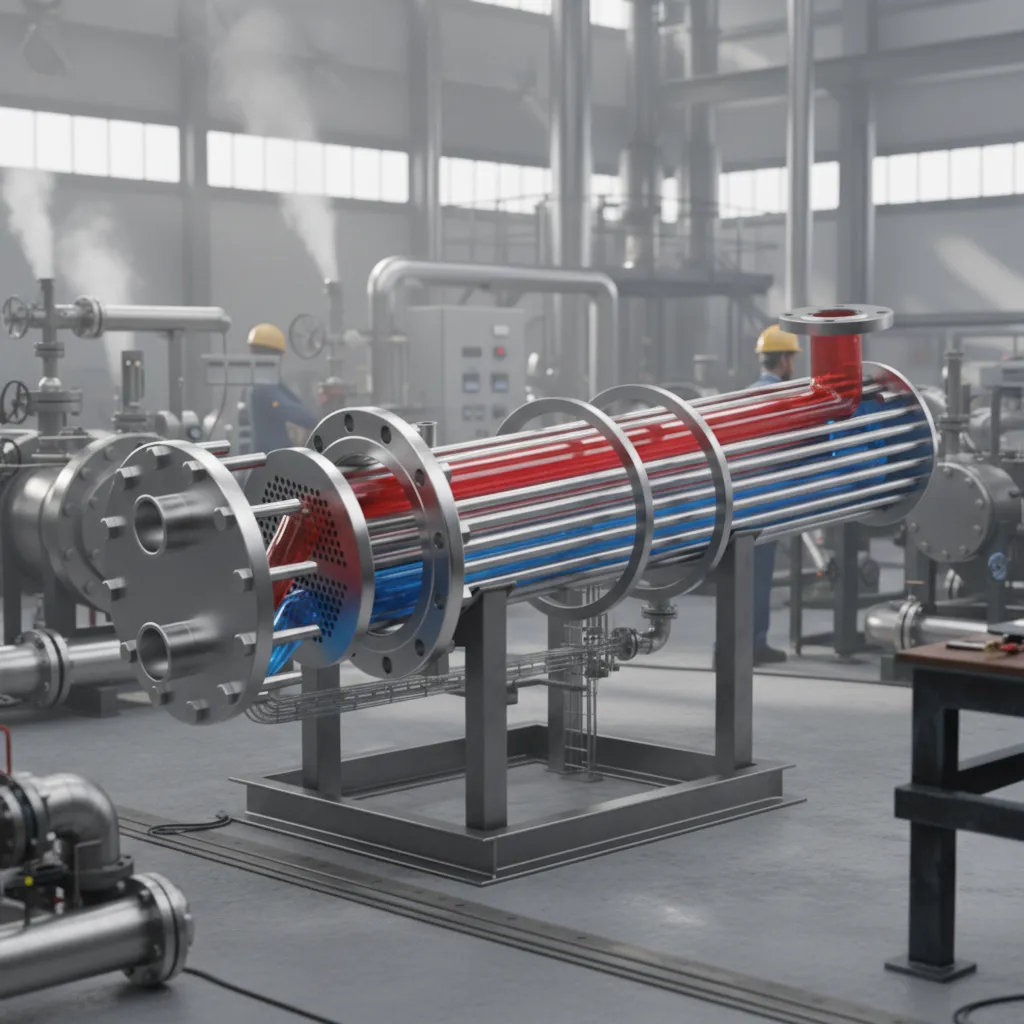
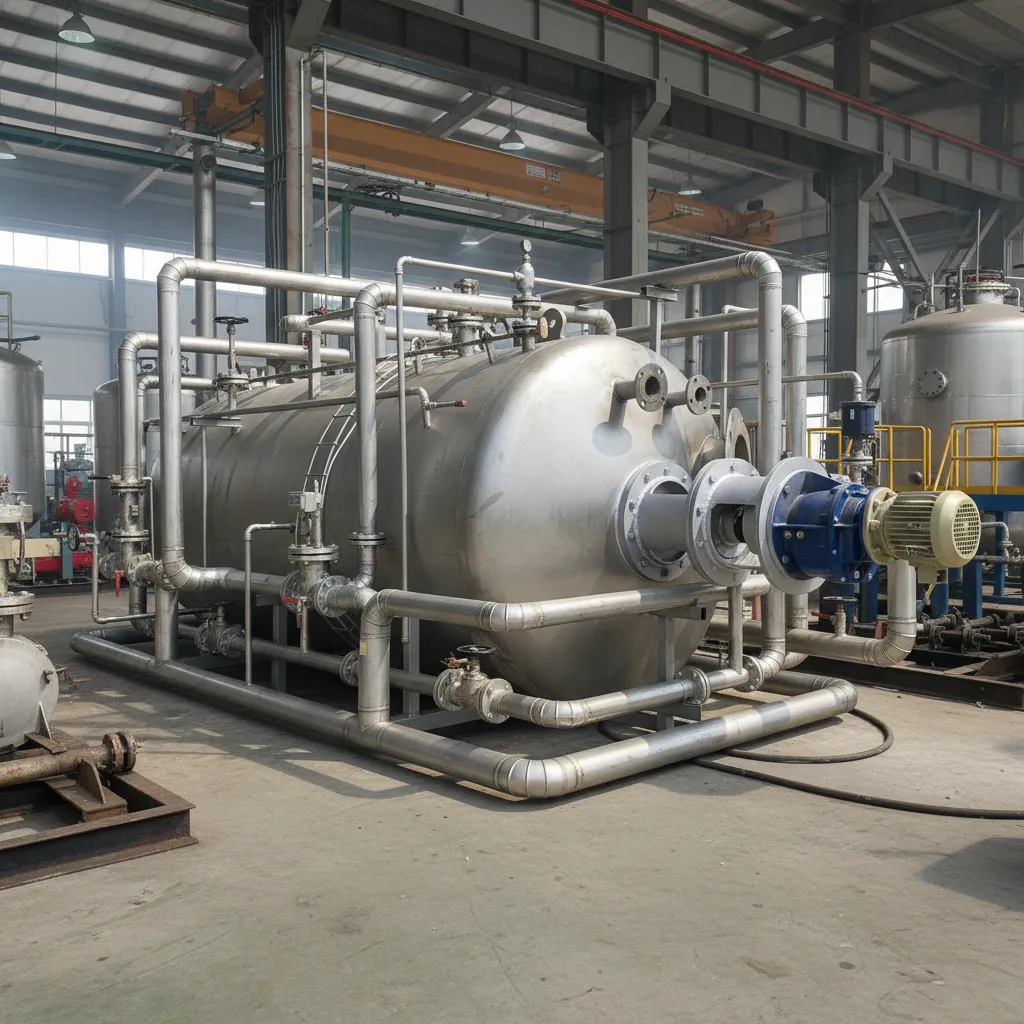
Our stainless steel chemical reactors are engineered for controlled chemical reactions, mixing and processing in the pharma, chemical and specialty industries. With jacketed heating / cooling, agitation systems and corrosion-resistant SS construction, these reactors deliver precise, safe and consistent reaction control across batch and continuous processes.

Key Features

Precise Control

Accurate temperature and reaction control.

Jacketed Design

Heating / cooling jacket or limpet coil.

Efficient Agitation

Motorized stirrer for uniform reaction.

Corrosion Resistant

SS304 / SS316 resists chemicals.

Pressure Rated

Built for pressure and vacuum service.

Safety Fittings

Valves, gauges and safety devices.

Manufacturing Process

01

Design & Engineering

Custom design and drawings prepared as per specifications.

02

Material Selection

High-grade SS / MS material selected for the application.

03

Cutting & Forming

Plates cut, rolled and formed to the required shape.

04

Welding & Fabrication

Precision welding and assembly by skilled technicians.

05

Quality Testing

Dimensional, leak and pressure tests for assurance.

06

Surface Finishing

Polishing, coating or treatment for durability.

07

Dispatch & Installation

Safe delivery and on-site installation support.

Technical Specifications

Capacity Range 50 L to 20 KL (customizable)
Material SS304 / SS316
Jacket Limpet / conventional / coil
Agitator Anchor / paddle / turbine
Design Pressure / vacuum rated
Heating Steam / oil / electric
Application Chemical reactions

Benefits

Precise Reactions

Tight control delivers consistent output.

Corrosion Free

SS body handles aggressive chemicals.

Efficient Heating

Jacket / coil enables fast heat transfer.

Versatile Use

Suits a wide range of processes.

Safe Operation

Rated and tested for safe service.

Durable

Robust build for demanding duty.

Industry Applications

  • Pharmaceutical
  • Chemical Industry
  • Specialty Chemicals
  • Cosmetics
  • Agrochemicals
  • Resin & Polymer

Why Choose Shree Narayan Engineering Pvt. Ltd.

01

Industry Experience

Years of expertise in industrial equipment fabrication.

02

Customized Solutions

Built to your exact specifications and requirements.

03

Quality Materials

Premium SS / MS grades for durability and performance.

04

Turnkey Support

Complete service from design to installation.

05

After-Sales Service

Reliable maintenance and technical assistance.

06

Competitive Pricing

Cost-effective solutions with strong value.

FAQs

Stainless Steel Chemical Reactor FAQs

We build stainless steel chemical reactors from 50 L to 20 KL, and this capacity range is customizable. Each reactor starts with custom design and drawings prepared as per your specifications, so it can be built to your exact requirements for batch or continuous processes.
We fabricate stainless steel chemical reactors in SS304 or SS316. Both grades give corrosion-resistant SS construction, and the SS body handles aggressive chemicals used in pharma, chemical and specialty industry processing. The grade is selected to suit your application.
We offer a heating and cooling jacket in limpet, conventional or coil form, with steam, oil or electric heating. For mixing, a motorized stirrer with an anchor, paddle or turbine agitator gives uniform reaction. Together these support accurate temperature and reaction control during processing.
Yes. Our stainless steel chemical reactors are pressure and vacuum rated and are fitted with valves, gauges and safety devices. Our manufacturing process includes dimensional, leak and pressure tests for assurance. The design is prepared as per your specifications, so please share your operating pressure or vacuum and temperature when you send an inquiry.
Yes. Our stainless steel chemical reactors are engineered for controlled chemical reactions, mixing and processing in pharmaceutical, chemical, specialty chemicals, cosmetics, agrochemicals, and resin and polymer applications. Tight temperature and reaction control delivers consistent output, and the reactor suits a wide range of processes.
We quote each stainless steel chemical reactor per project, based on the capacity and specification you need, such as volume, SS grade, jacket, agitator and heating. Send your requirement through the inquiry form on this page or the Get a Quote page, or call +91 81560 60100, Monday to Friday, 10:00 am to 7:30 pm.
Send an Inquiry

Interested in Stainless Steel Chemical Reactor?

Share your requirement and our team will get back to you with details, specifications and a tailored quote.