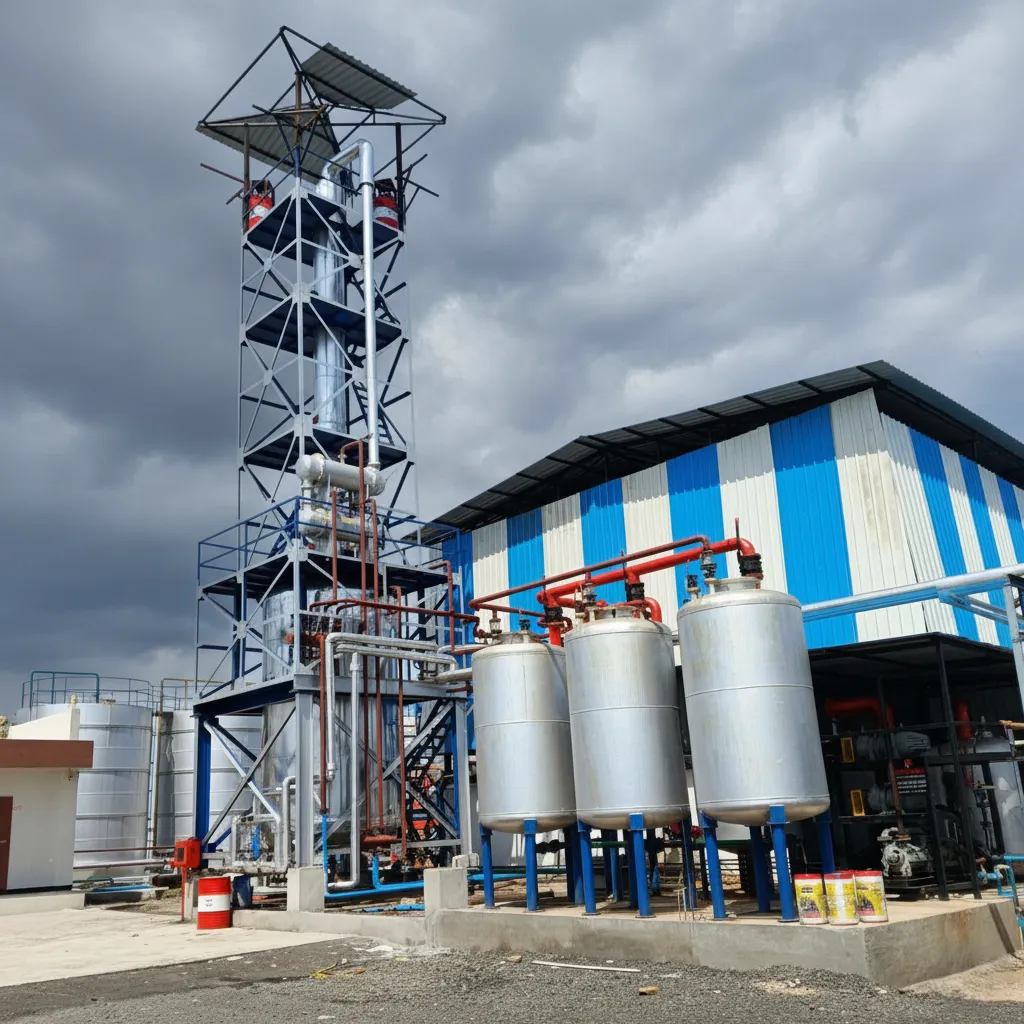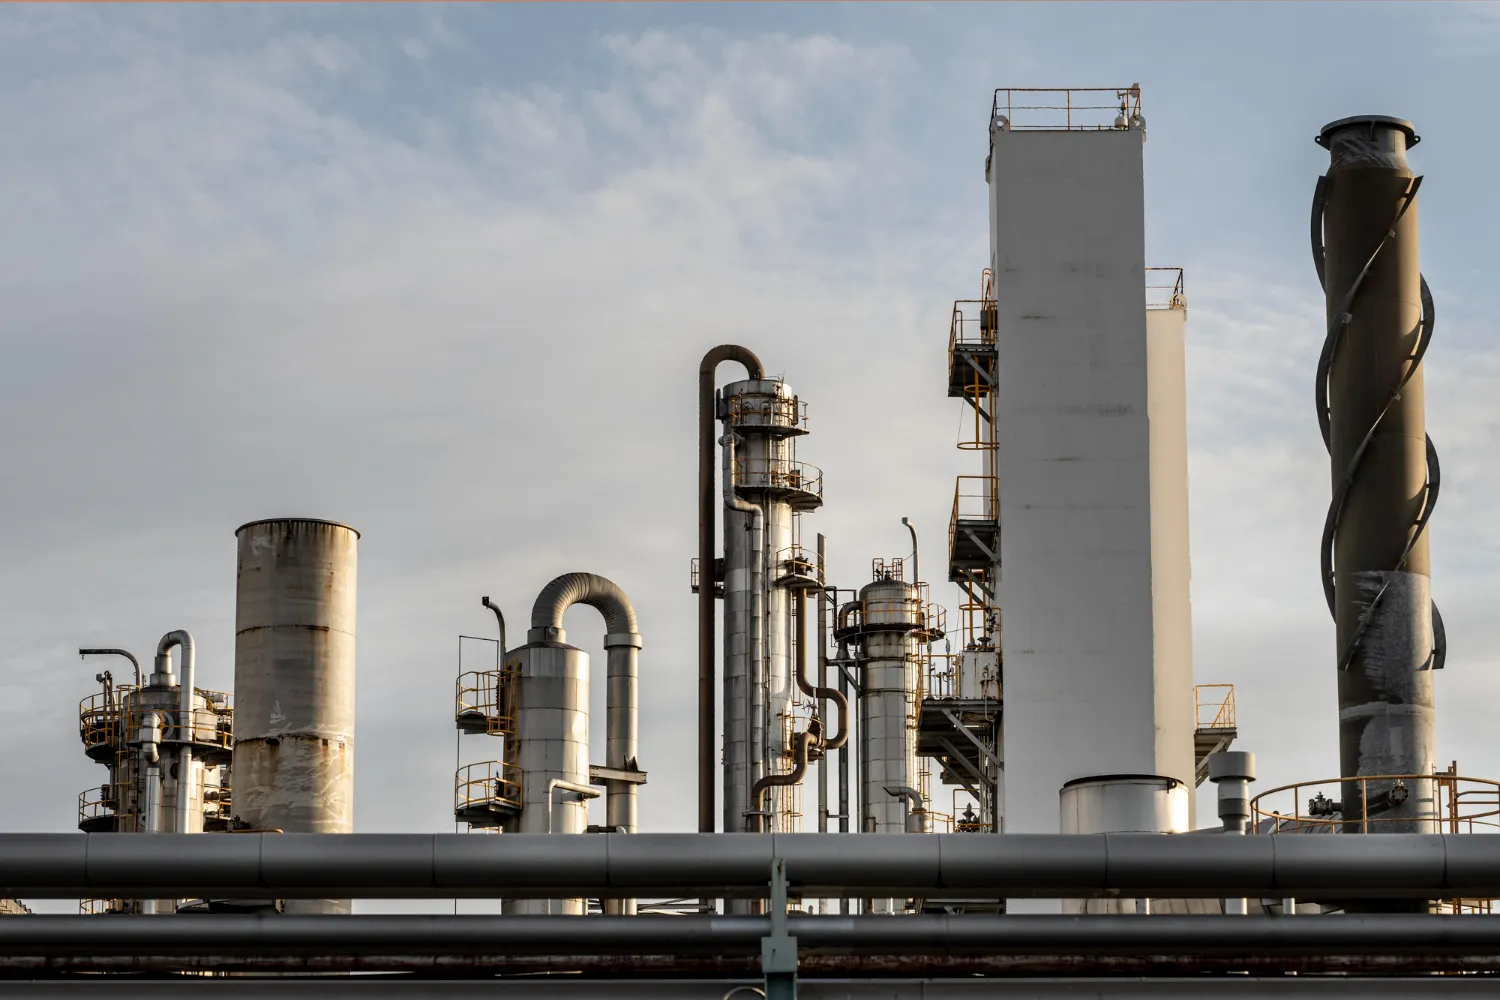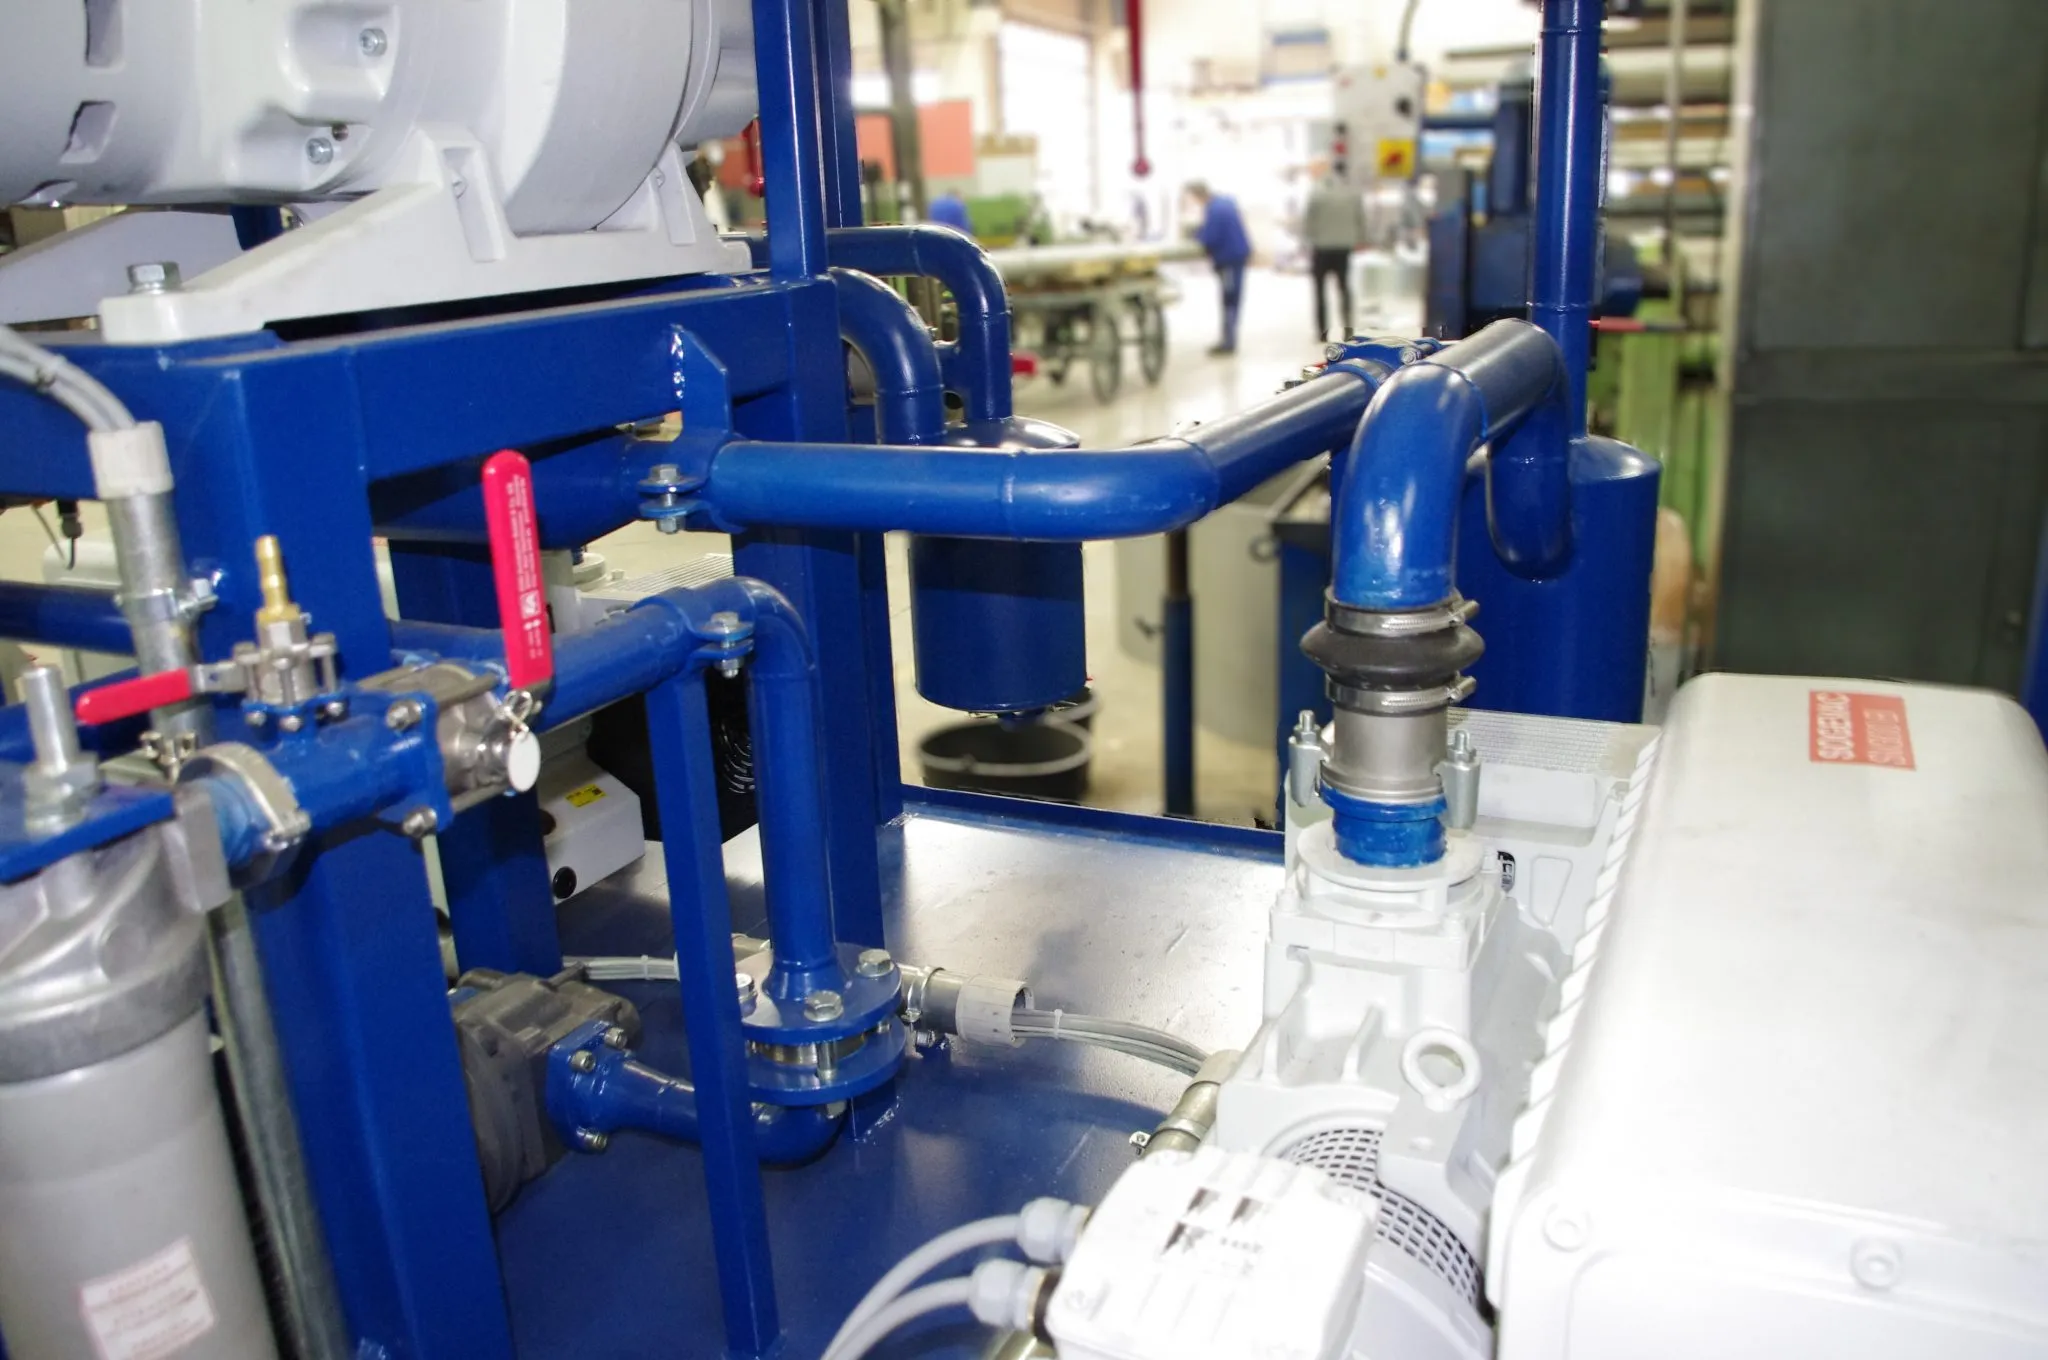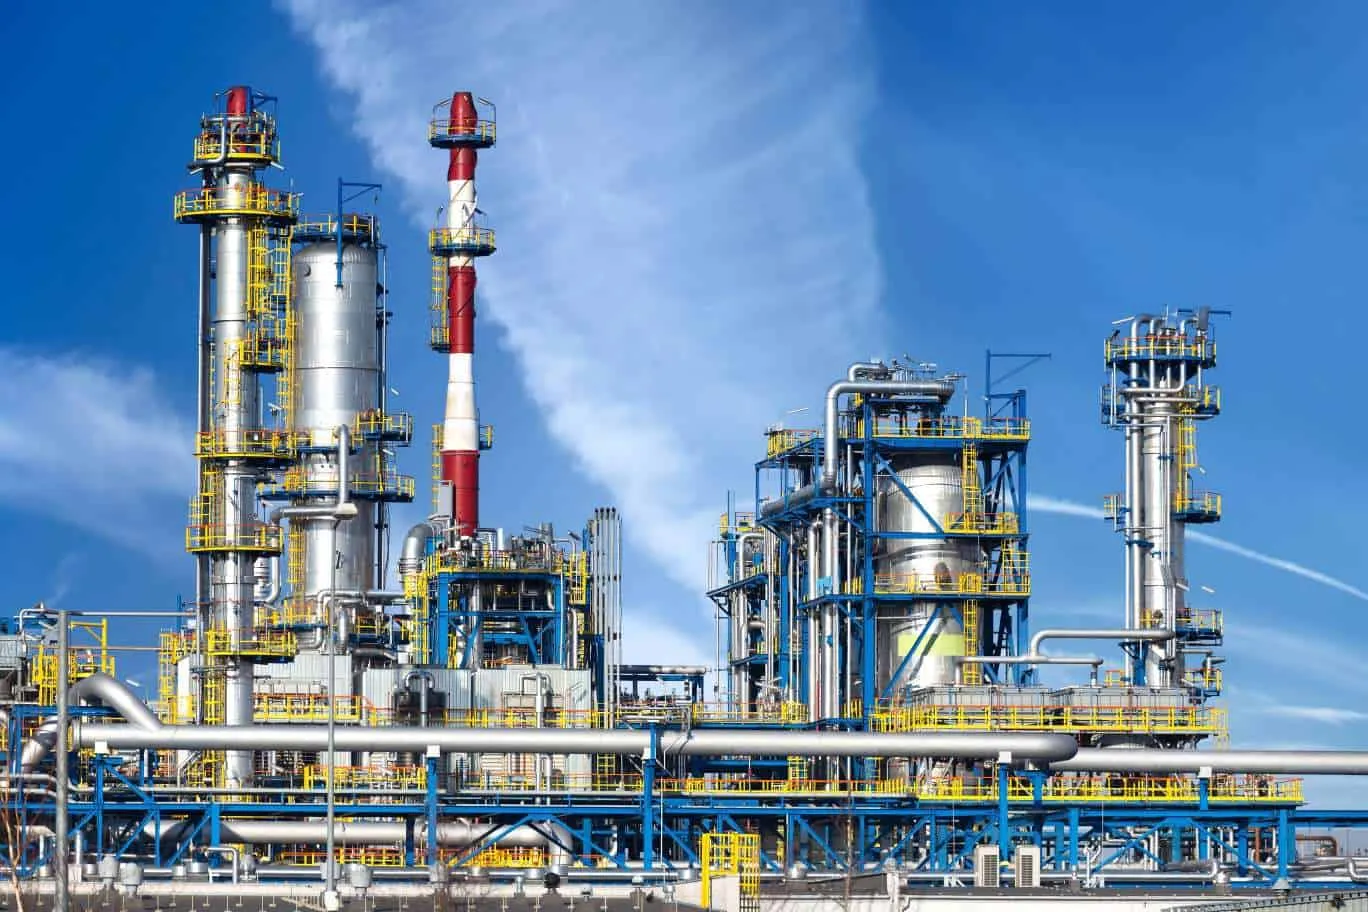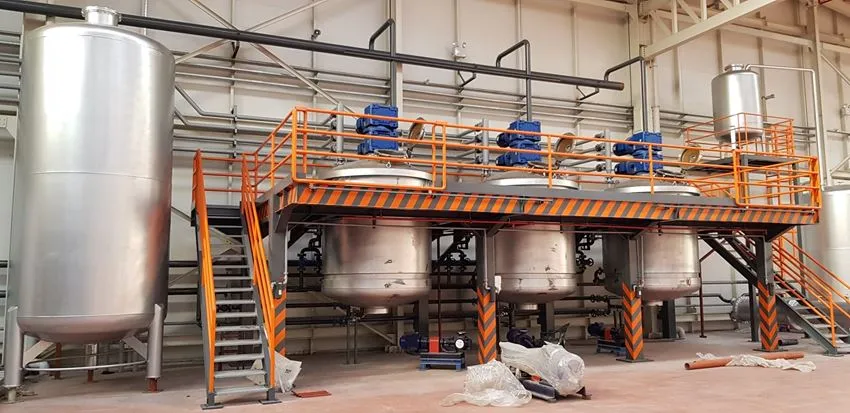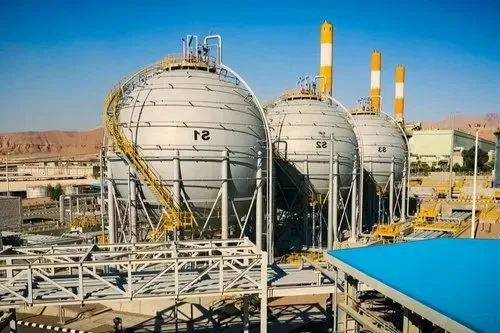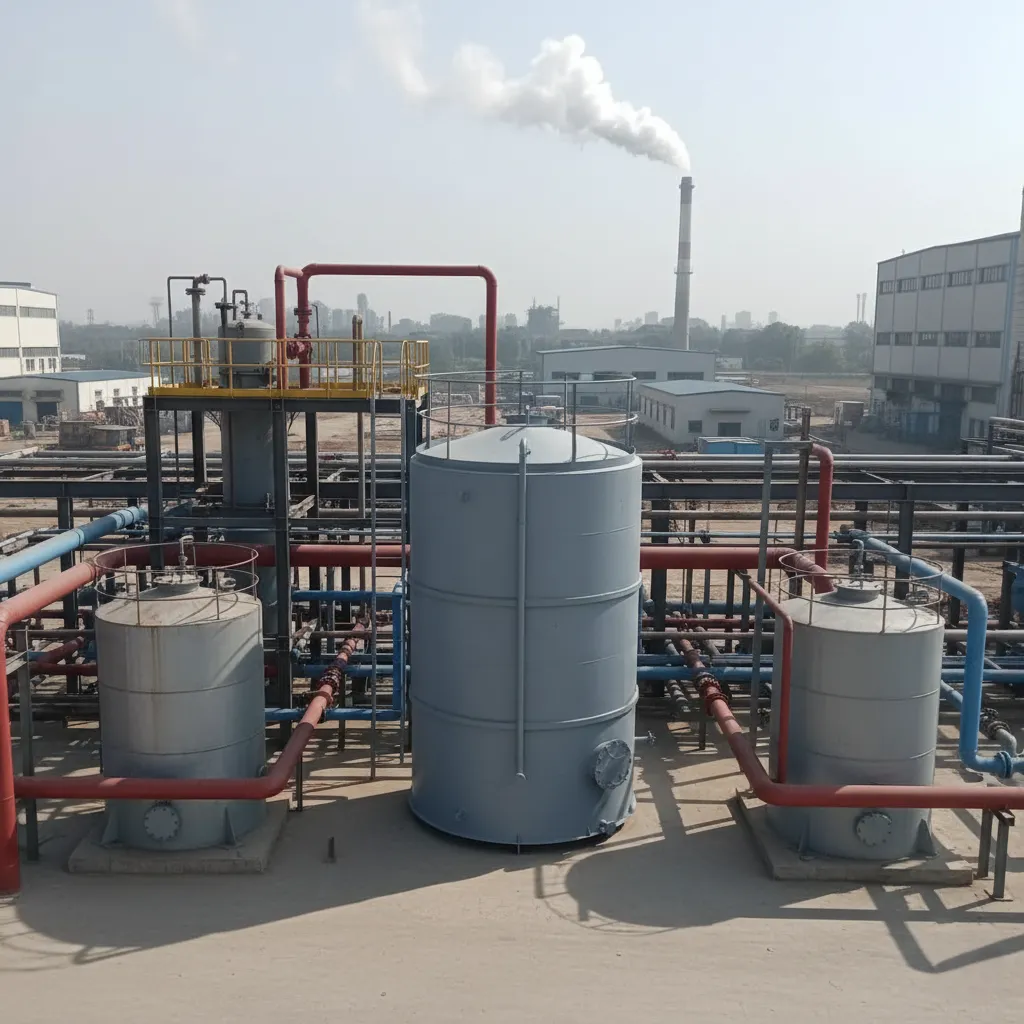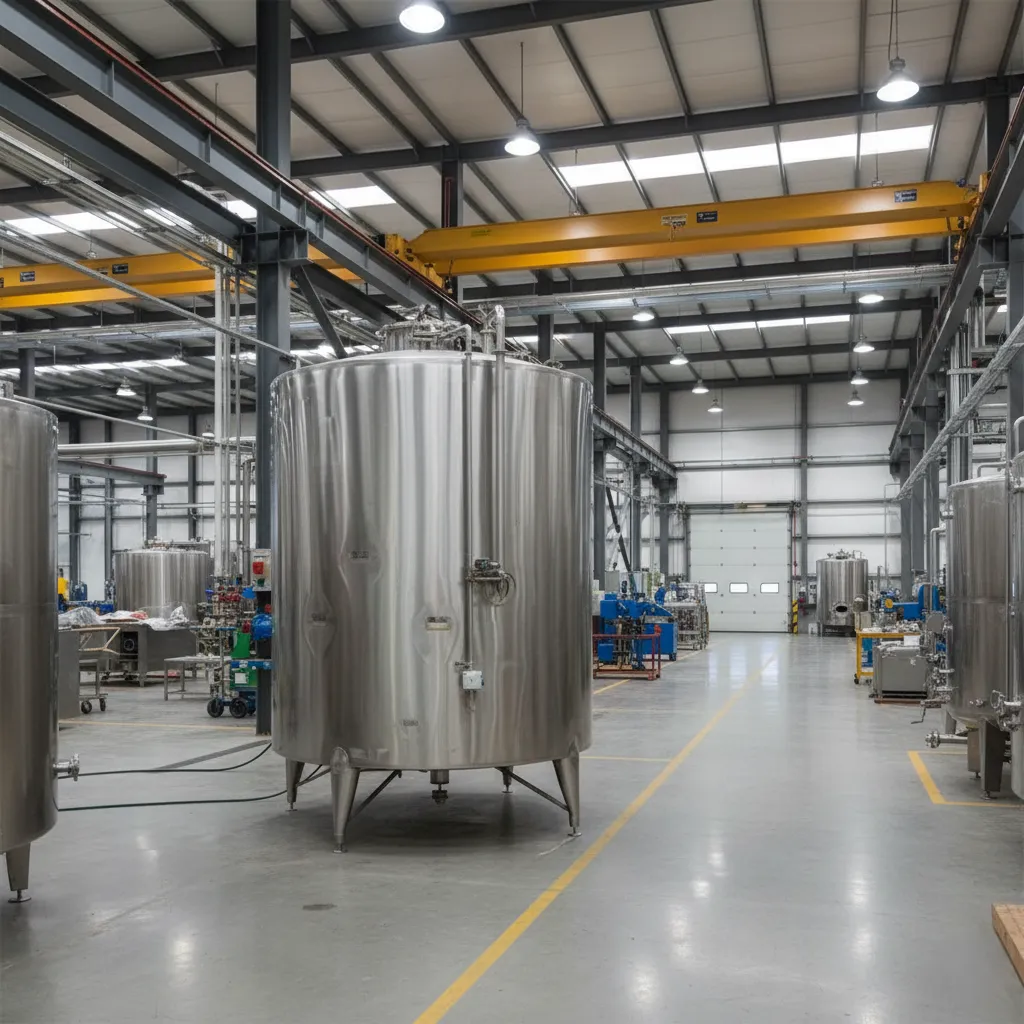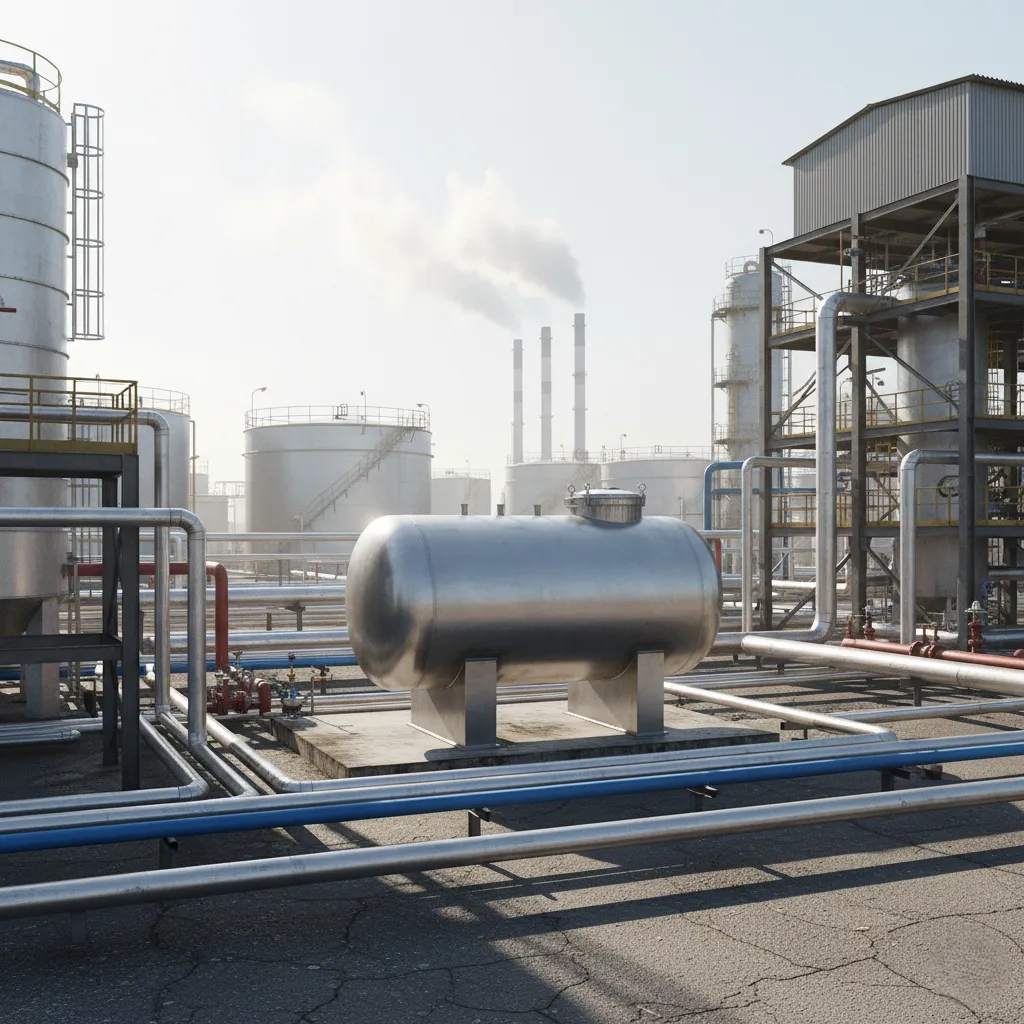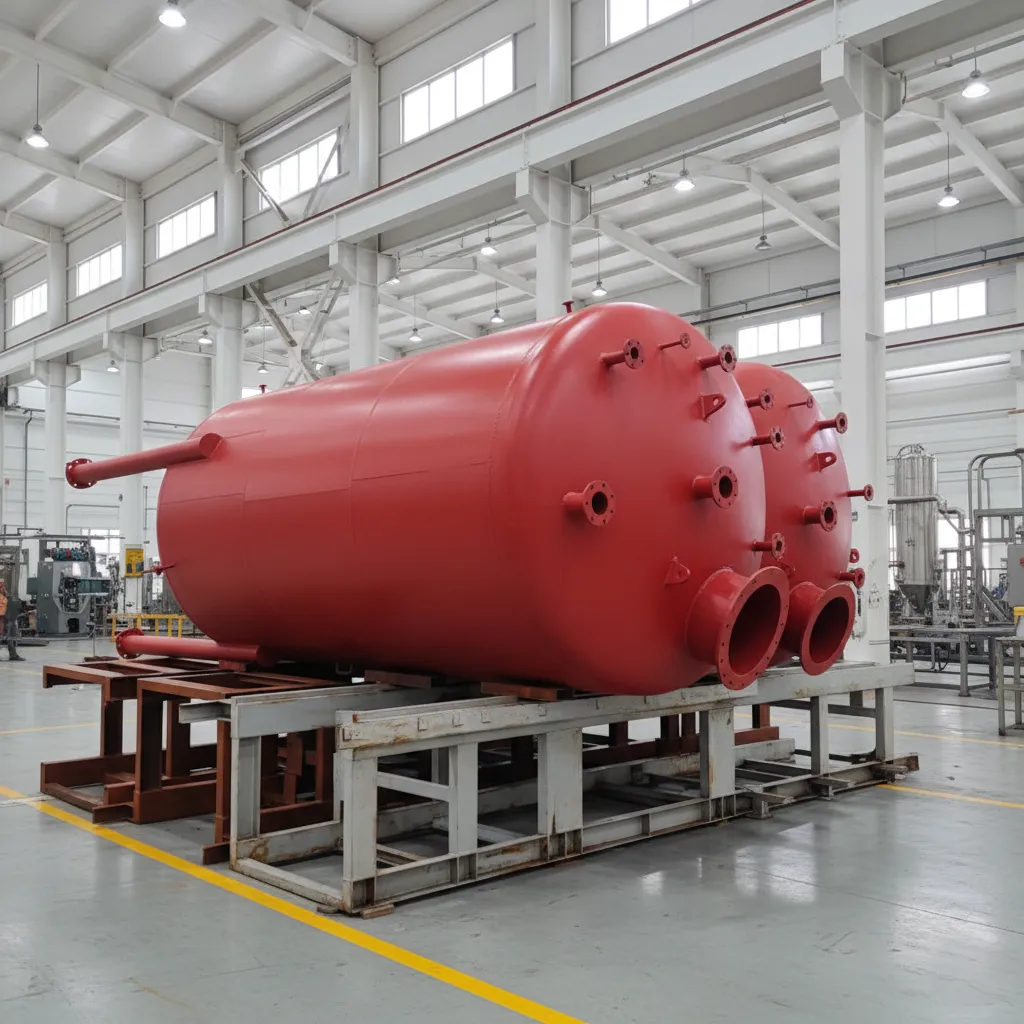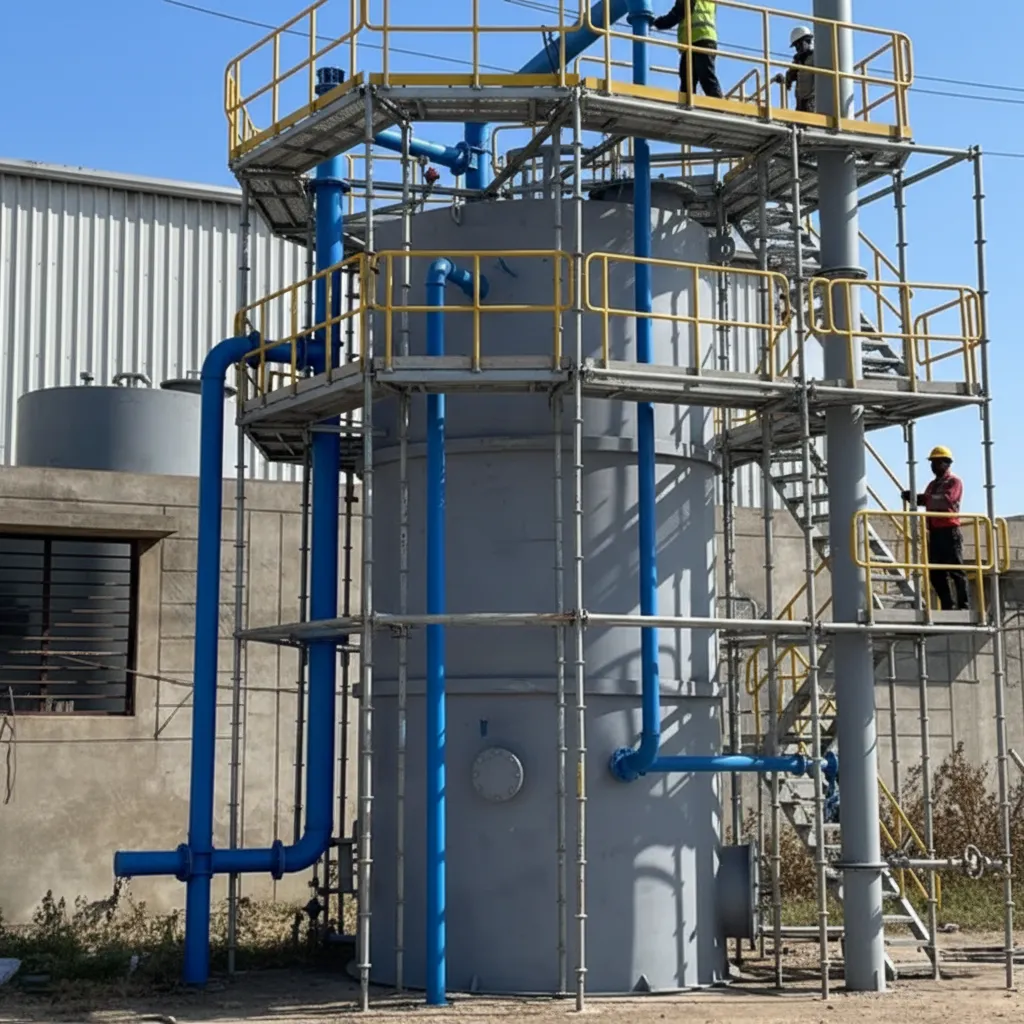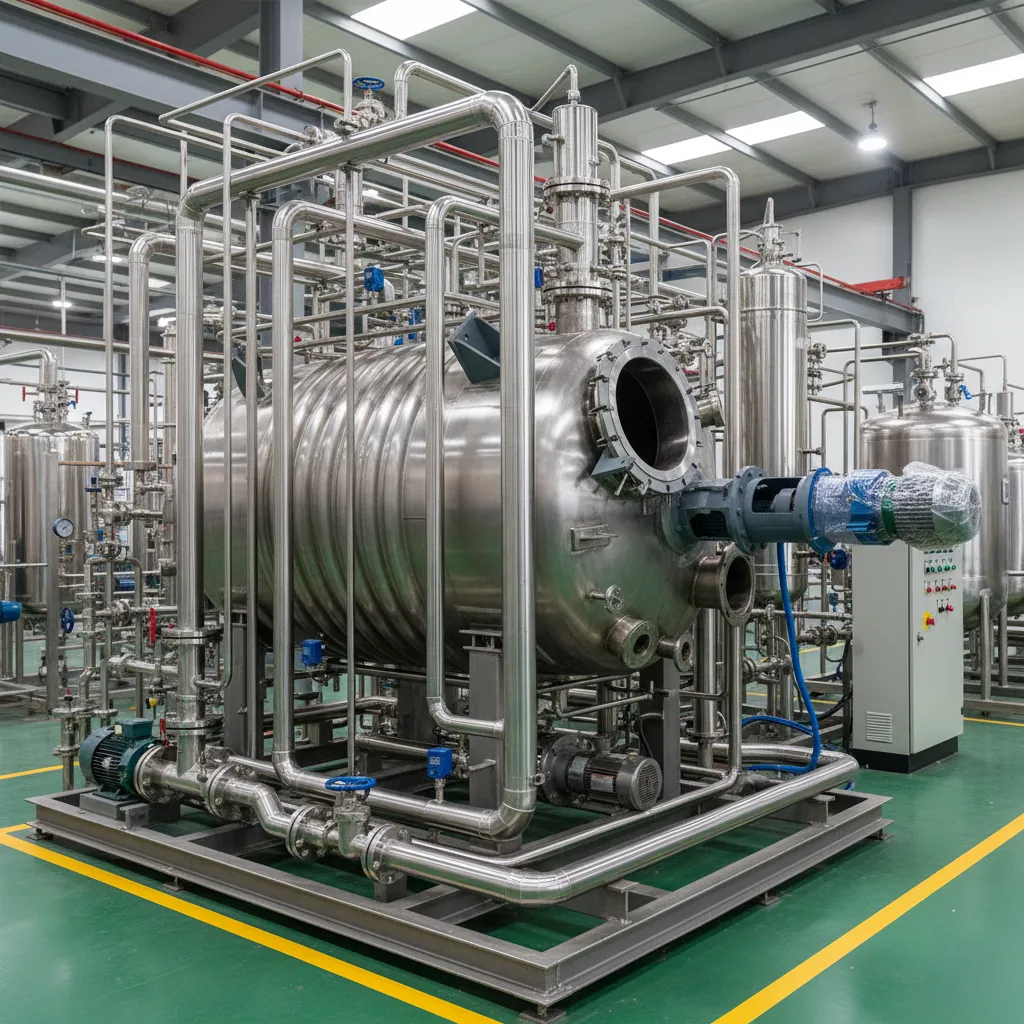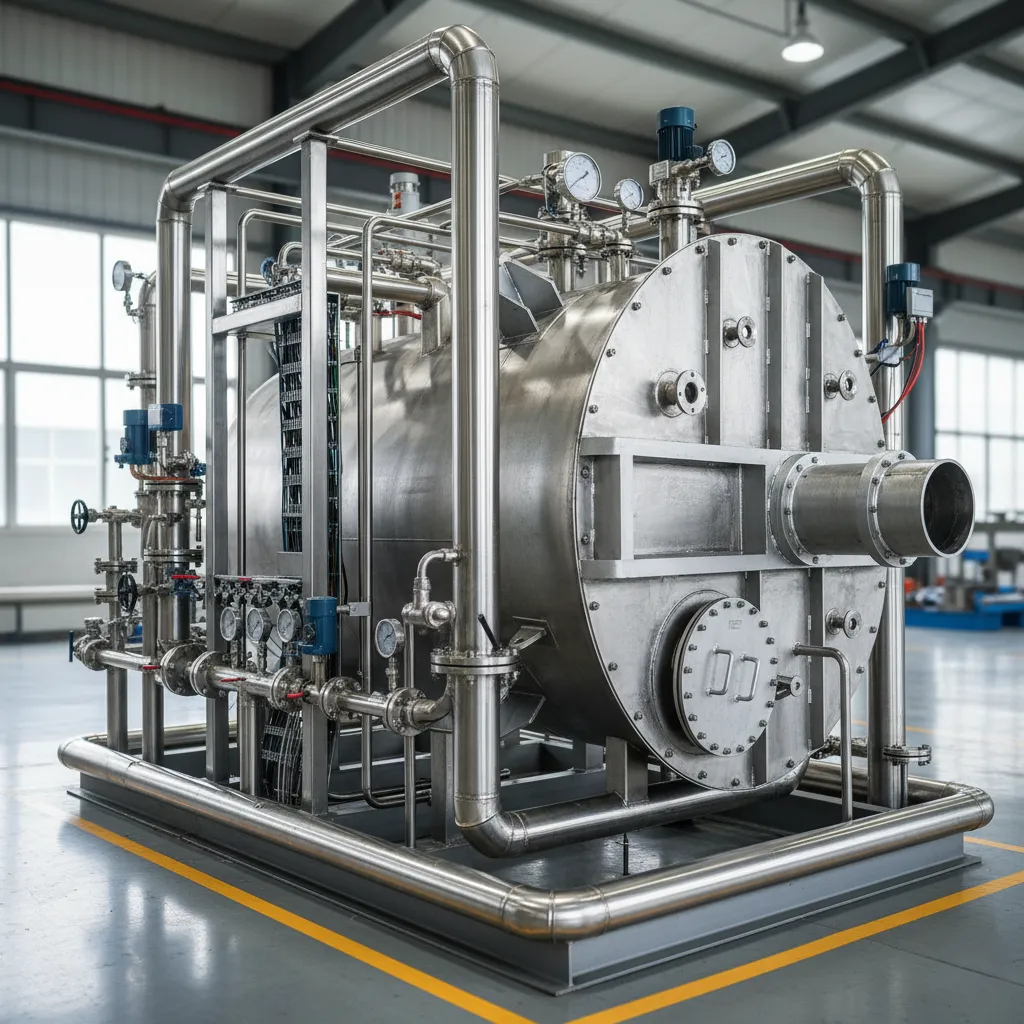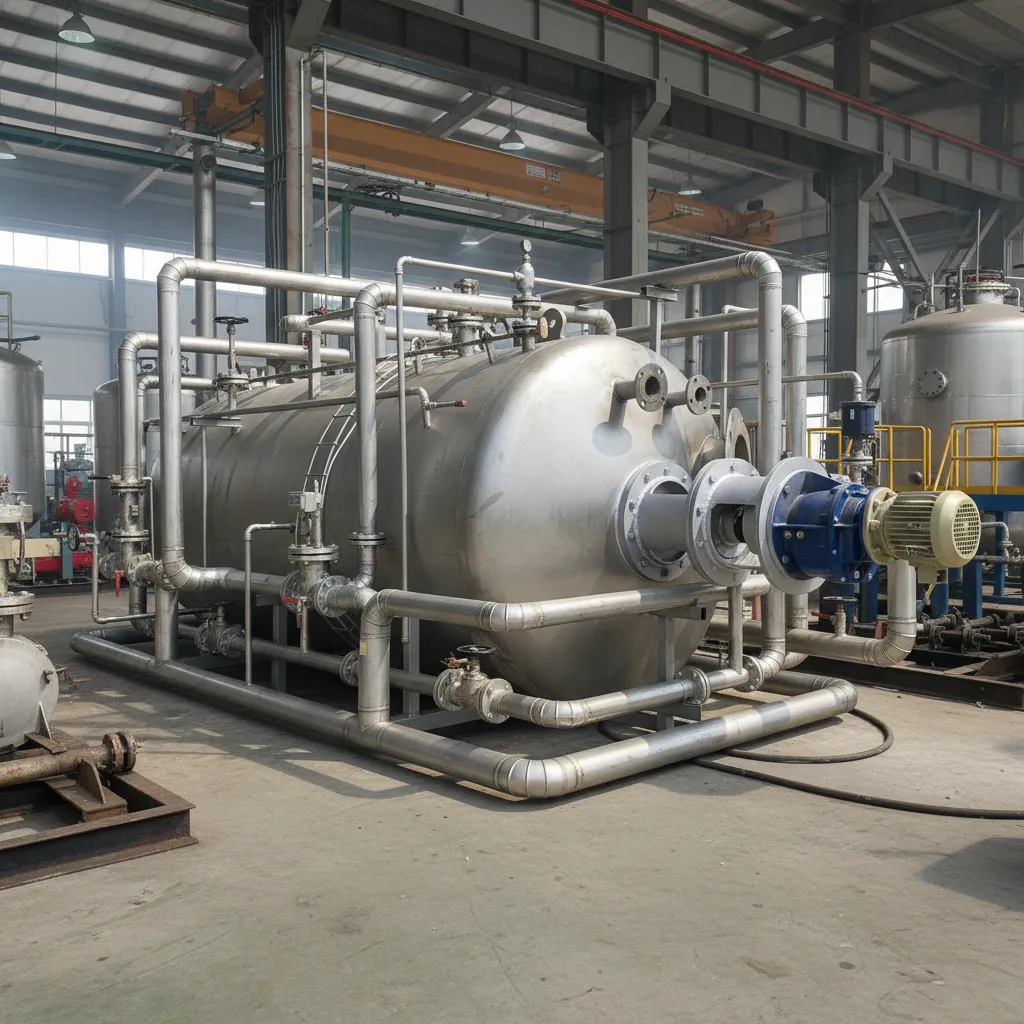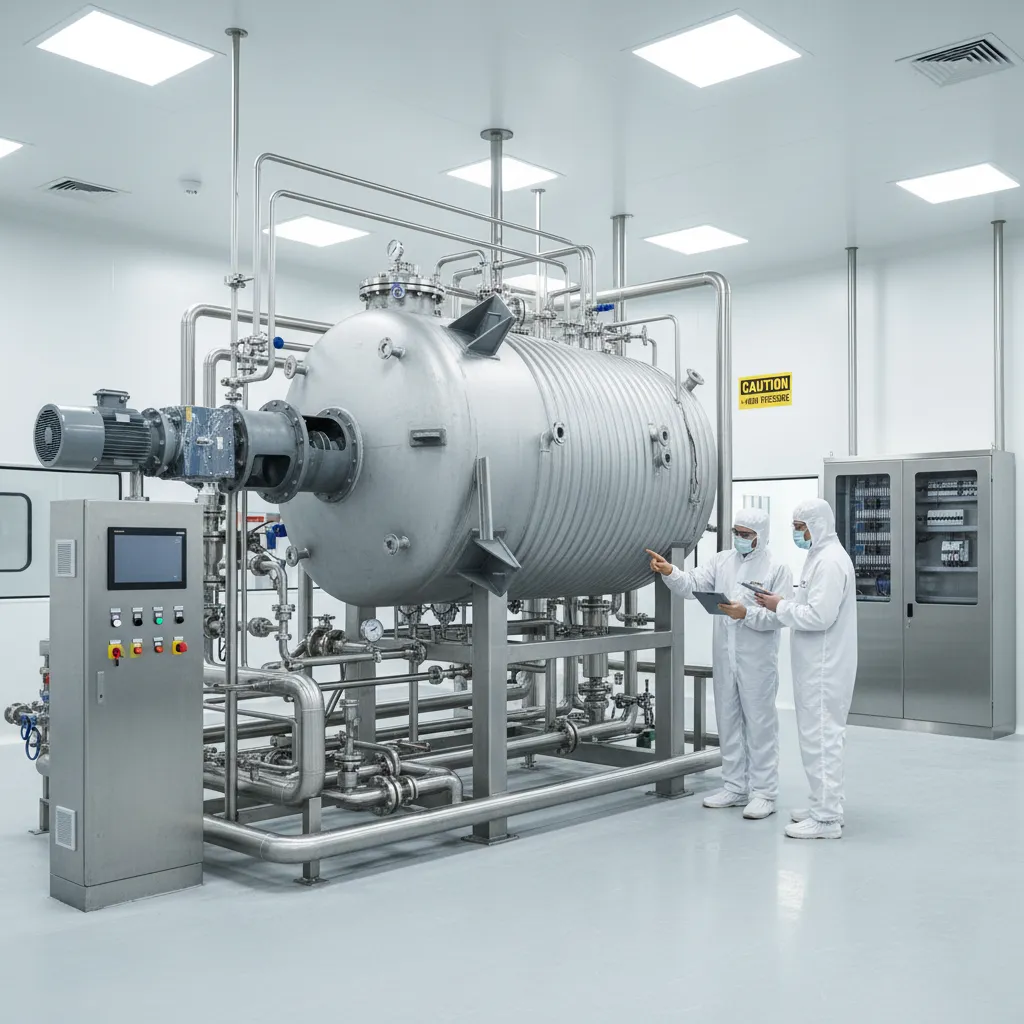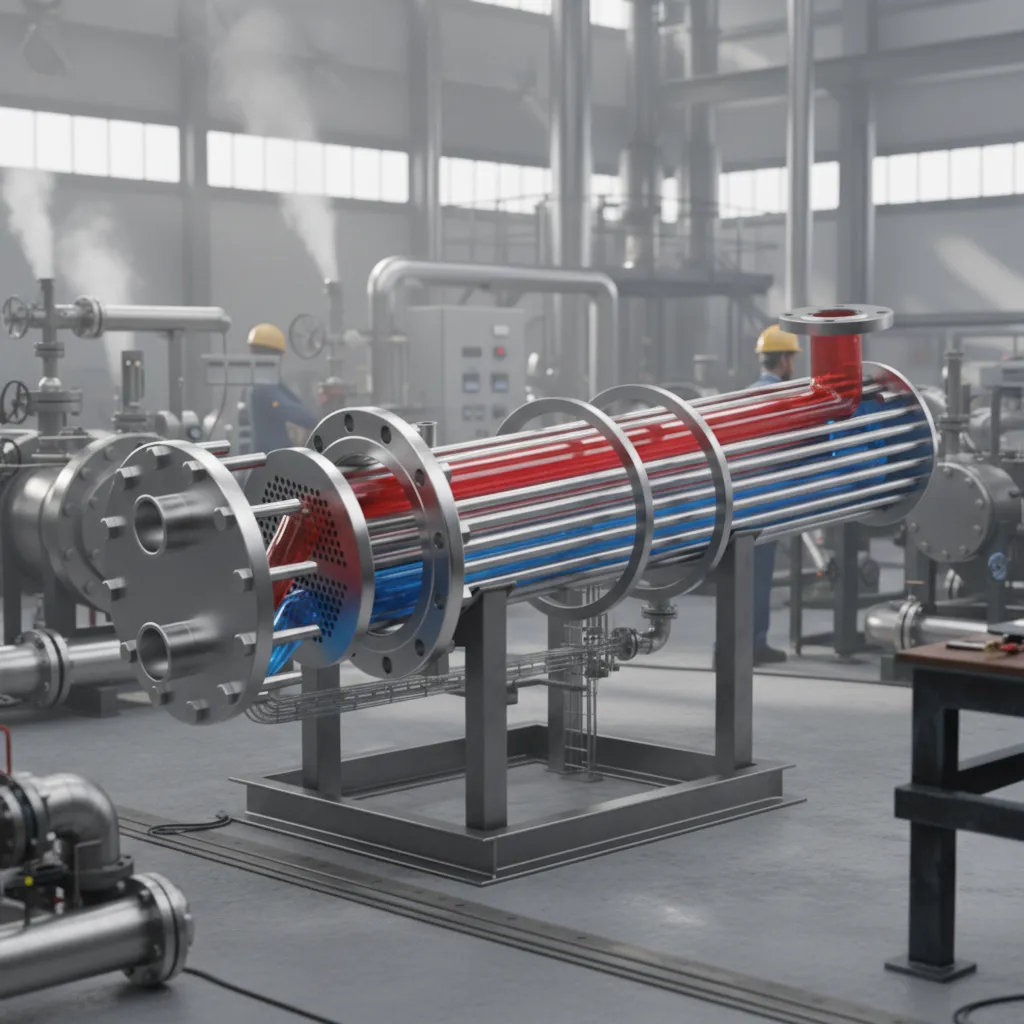
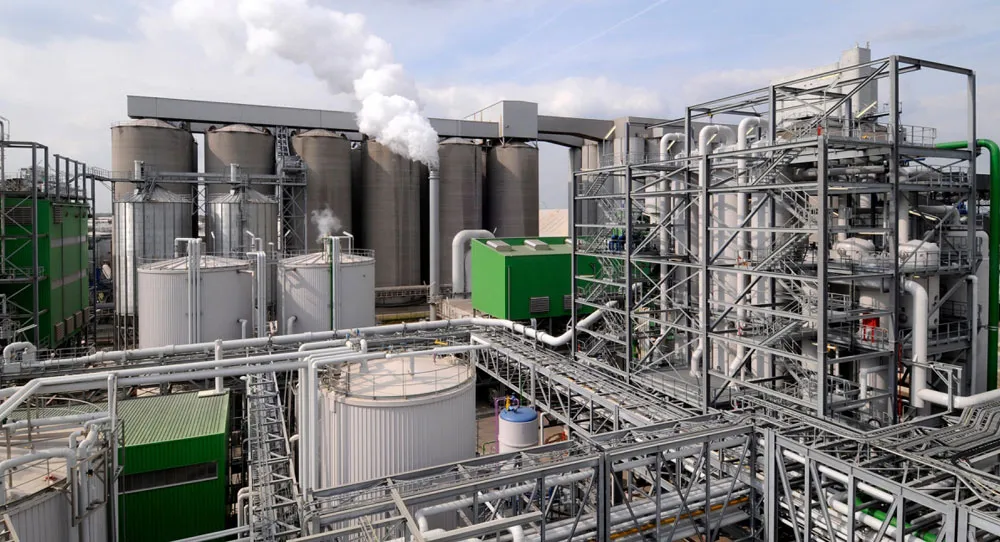
Efficient distillation plant solutions for separating and purifying liquids with high-purity output across multiple industries.
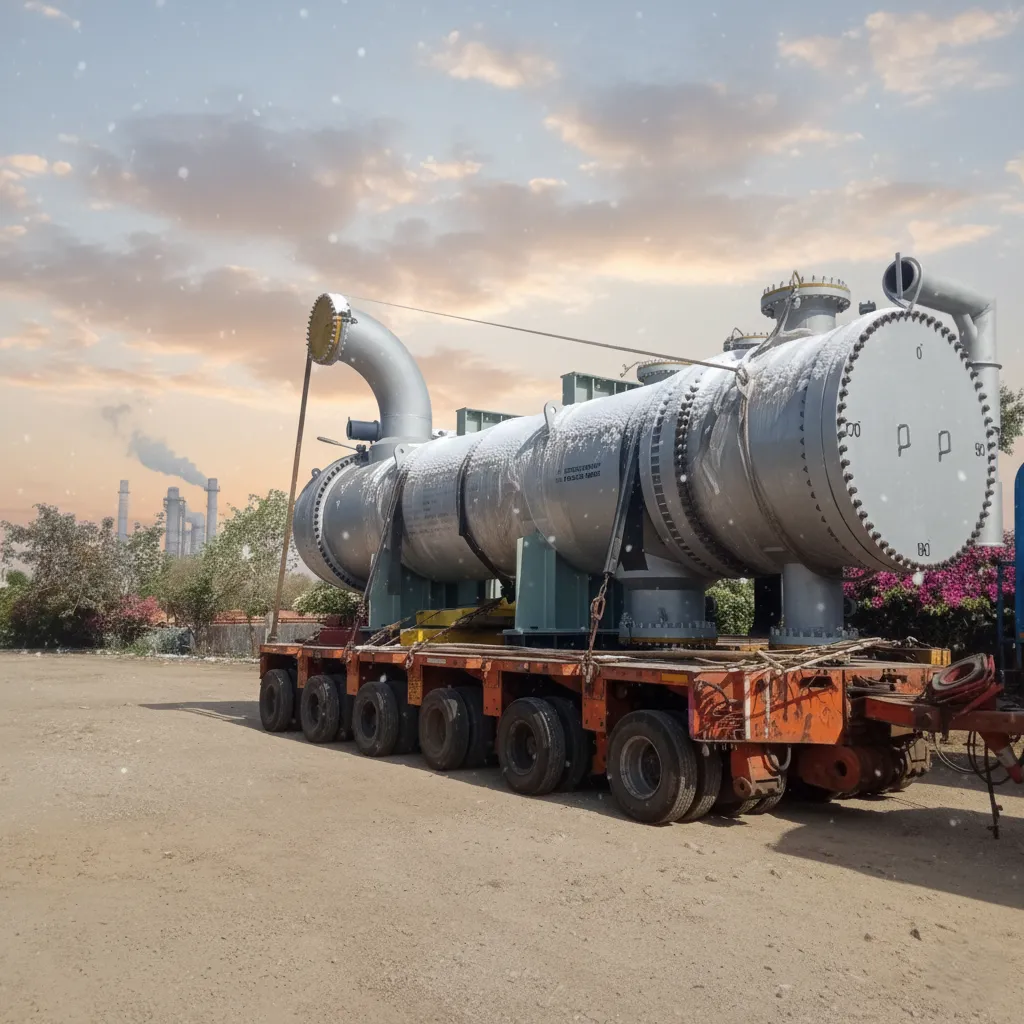
Shree Narayan Engineering Pvt. Ltd. is a leading distillation plant manufacturer providing efficient solutions for separating and purifying liquids in various industries. Our systems process different feedstocks and deliver high-purity output through controlled heating and condensation, serving chemical, pharmaceutical, petrochemical and alcohol production sectors with reliable automation and energy-efficient operation across small to large-scale production.
PLC / SCADA-based systems ensure accurate monitoring and smooth plant operation.
Innovative distillation columns deliver precise separation and superior product quality.
Integrated heat recovery systems reduce energy consumption and operational costs.
Built with corrosion-resistant materials for long-term durability.
Supports both batch and continuous distillation processes.
Enables efficient separation of complex mixtures with low maintenance.
Liquid mixtures pre-treated to remove impurities before distillation.
Liquid converted to vapour inside the reboiler under controlled heat.
Vapours ascend through the distillation column.
Components separate according to their boiling points.
Separated vapours cooled back into liquid form.
Separated fractions collected and stored in tanks.
Unprocessed material reprocessed for improved efficiency.
| Capacity Range | 10 KLPD to 200 KLPD (customizable) |
|---|---|
| Feed Type | Chemical liquids, solvents, oils, alcohols |
| Automation Level | Semi-automatic / Fully automatic |
| Distillation Type | Batch / Continuous / Fractional |
| Material | SS304 / SS316 / Mild Steel |
| Control System | PLC / SCADA based |
| Output Quality | High-purity industrial-grade products |
Precise separation delivers superior, consistent product quality.
Optimized distillation with minimal losses and waste.
Heat recovery reduces energy use and operating costs.
Accurate monitoring and smooth, hands-off control.
Modular setup allows easy future expansion.
Durable construction ensures minimal downtime.
Extensive expertise in distillation plant manufacturing.
Plants designed to your exact process requirements.
Advanced systems for better output and efficiency.
Complete project support from design to commissioning.
Reliable maintenance and technical assistance.
Cost-effective solutions with strong ROI.
Share your requirement and our team will get back to you with details, specifications and a tailored quote.
Shree Narayan Engineering Pvt. Ltd. designs and manufactures sustainable industrial plant solutions with 15+ years of engineering expertise.
Copyright © Shree Narayan Engineering Pvt. Ltd. All Rights Reserved. | Designed & Developed by Clientsnow Technologies
Shree Narayan Engineering Pvt. Ltd. designs and manufactures sustainable industrial plant solutions with 15+ years of engineering expertise.